
Washing Machine Drum Stamping Lines Running at Midea Jingzhou Plant
 Nov 17, 2026|
 View:24
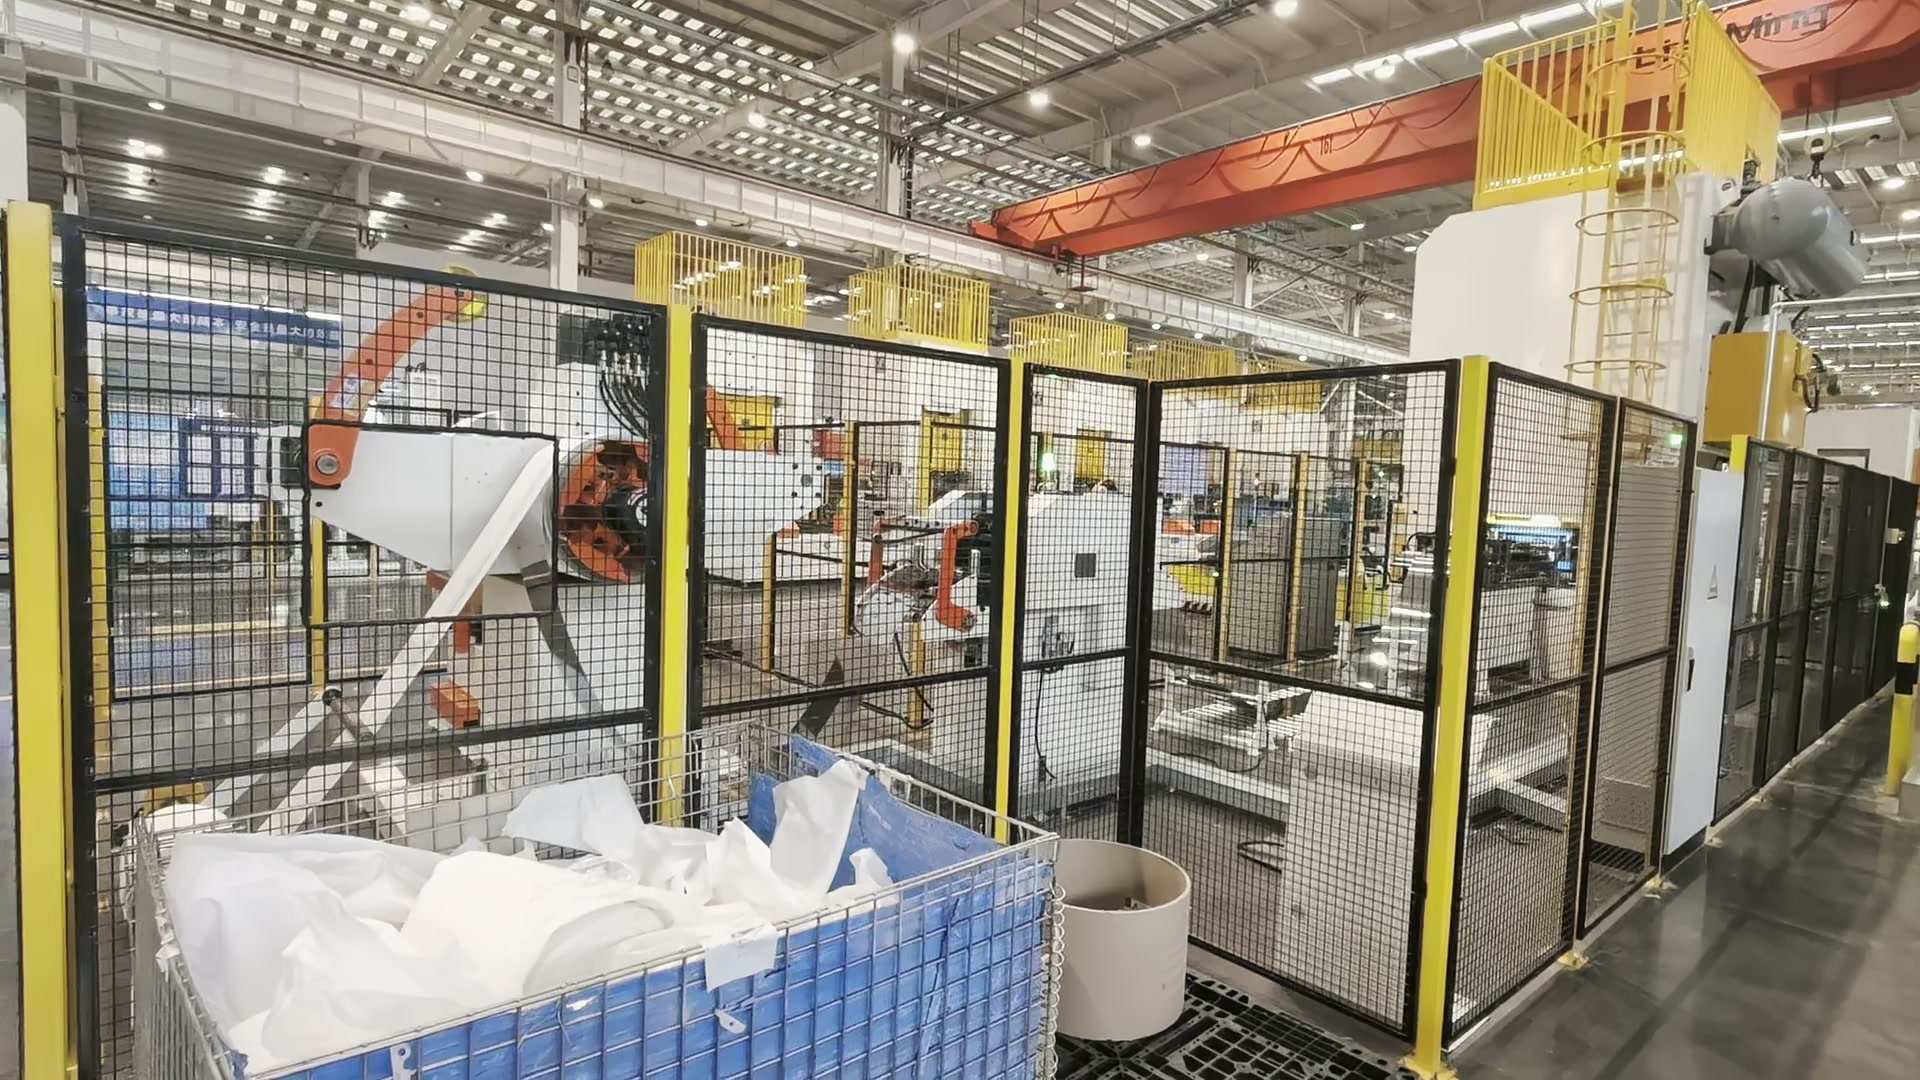
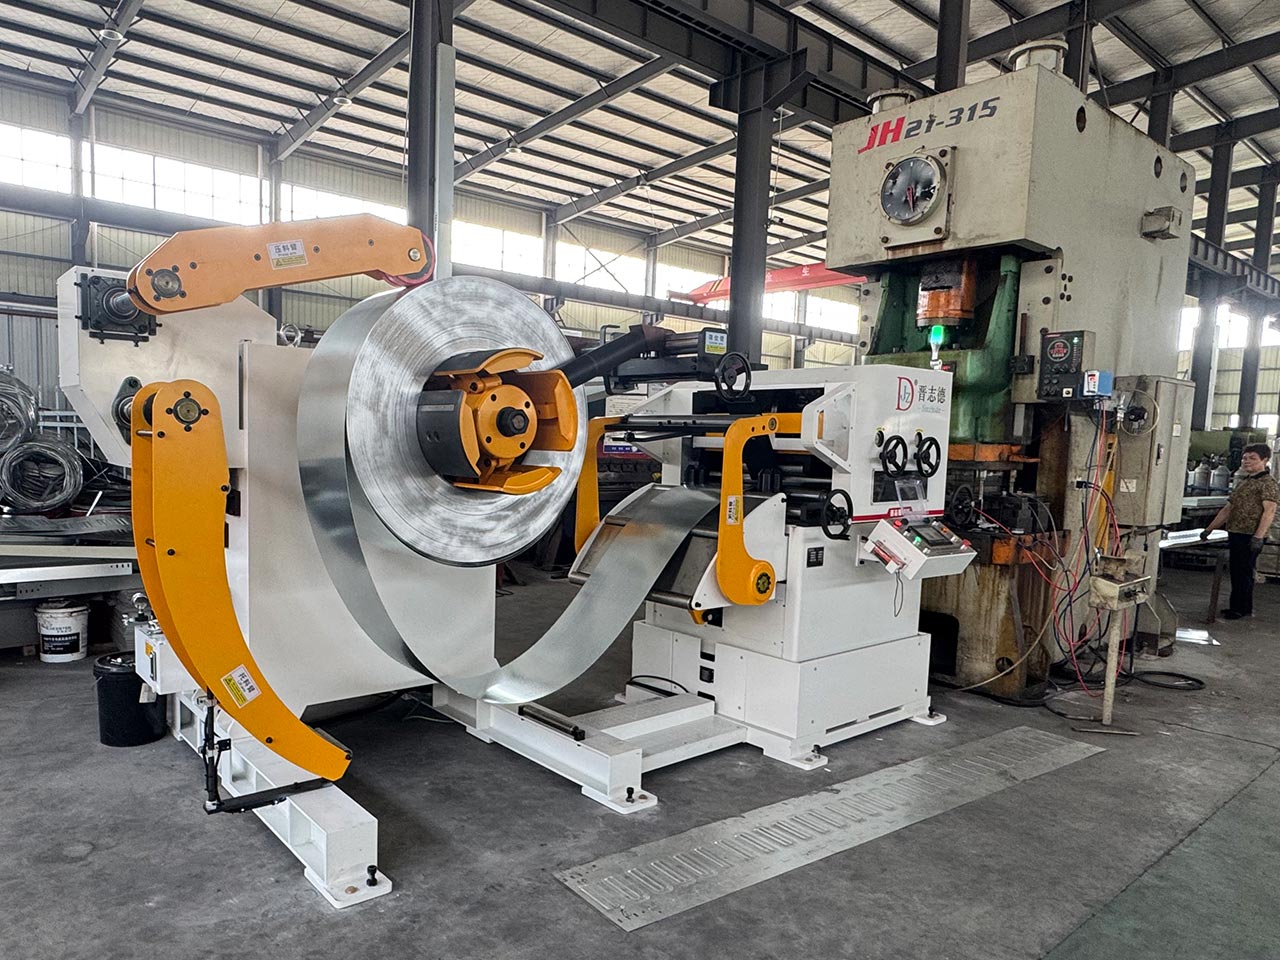
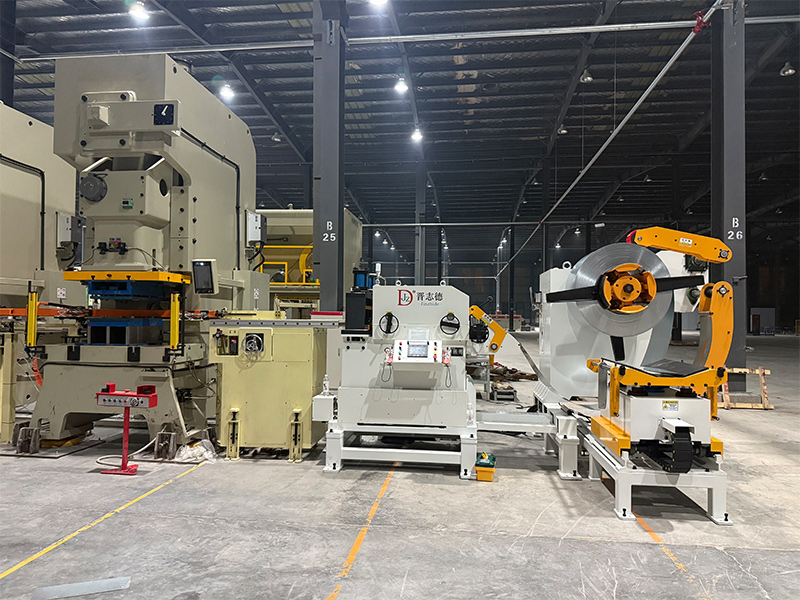
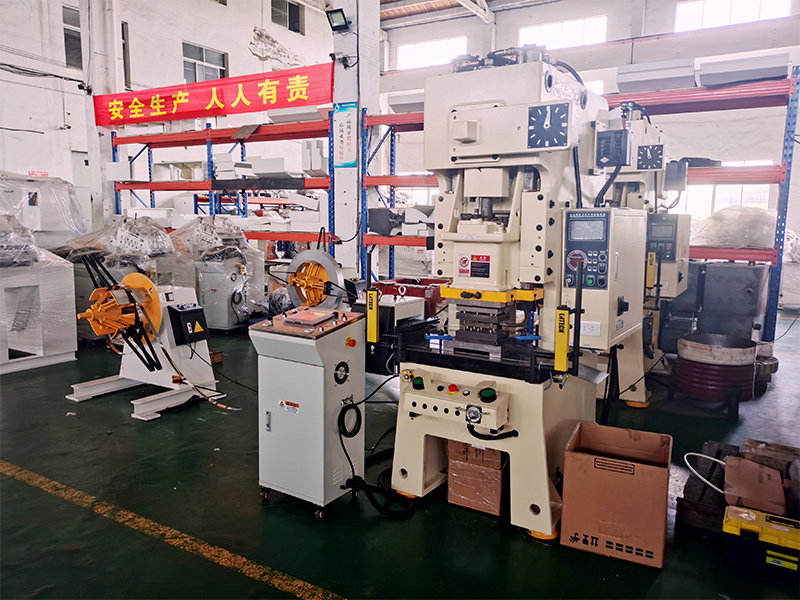
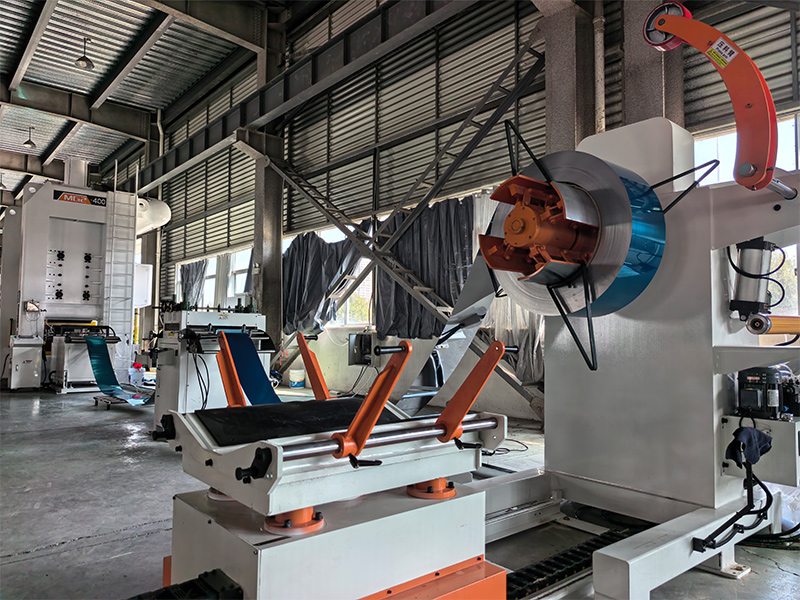
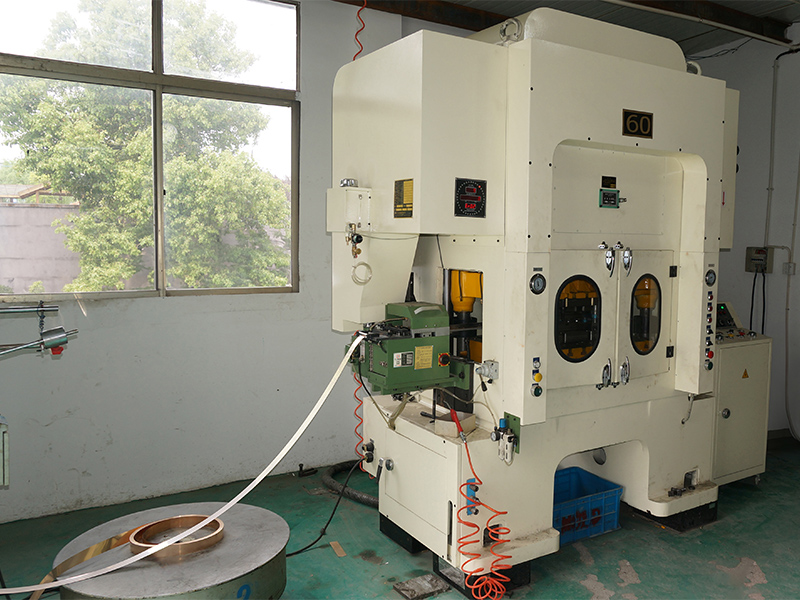
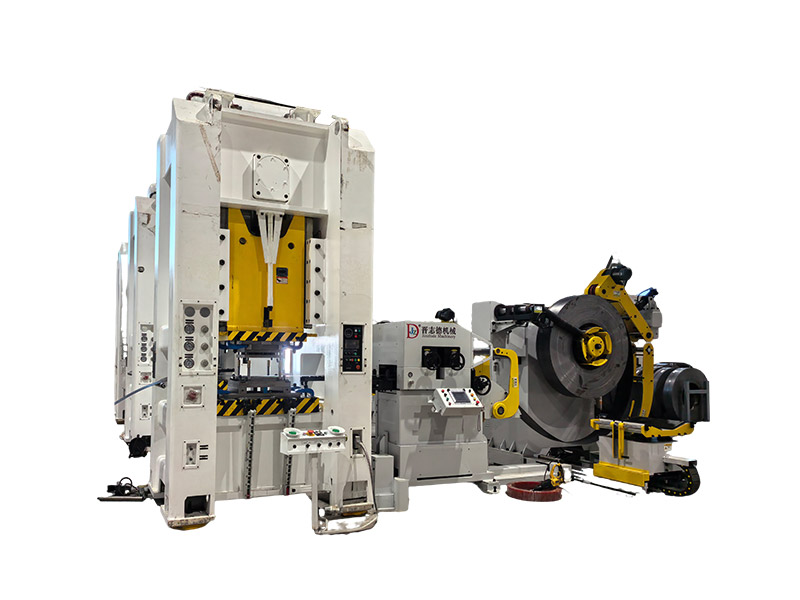
JINZHIDE has completed the installation and commissioning of two washing machine drum stamping lines at Midea's Jingzhou factory in China. Both production lines are now in operation, producing stamped steel sheets for washing machine inner drum manufacturing. Each line pairs a double head decoiler straightener with a servo gripper feeder, a 400 ton stamping press, and a progressive die, so steel coils travel from uncoiling to continuous stamping without manual sheet loading.
For appliance manufacturers, a washing machine drum stamping line is a coil-to-press system: the material stays in coil form until the die produces the sheet components. That arrangement removes manual sheet handling and keeps the press fed at a repeatable length. The sections below describe the equipment configuration of the two lines at Midea, how the double head decoiler straightener and the servo gripper feeder work together, and what data a factory needs before ordering a similar line.
Key Takeaways
Two washing machine drum stamping lines are running at Midea's Jingzhou factory, each built around a double head decoiler straightener, a servo gripper feeder, a 400 ton press, and a progressive die.
The double head design lets the next coil be prepared while the current coil is still being processed, which shortens the material change.
The servo gripper feeder advances the strip by a programmed distance and works in step with the press cycle.
Feed length, strip alignment, and press timing were checked during commissioning before production started.
Equipment selection starts with material data: strip width, thickness, coil weight, coil diameters, and the required feed length.
Washing Machine Drum Stamping Line Equipment Configuration
In a washing machine drum stamping line, the steel strip has to be straightened and fed into the die at the required length. Poor material flatness or an incorrect feed length affects the stamping process and the dimensions of the finished parts. The two washing machine drum stamping lines installed at Midea follow the same sequence, and the table below shows how each station contributes to it.
| Station | Equipment | Function in the line |
|---|---|---|
Coil preparation | Double head decoiler straightener | Holds two coils, unwinds the strip, and removes coil curvature before feeding. |
Feeding | Servo gripper feeder | Grips the strip and advances it by the programmed feed length. |
Stamping | 400 ton press with progressive die | Performs punching, cutting, and blanking through successive die stations. |
Output | Stamped steel sheets | Feed stock for washing machine inner drum forming. |
Instead of manually loading individual steel sheets into the press, a washing machine drum stamping line uses coil material for automatic feeding and continuous stamping. The feeder moves the strip forward according to the programmed length, and the press with its progressive die performs the required operations.
Double Head Decoiler Straightener for Faster Coil Preparation
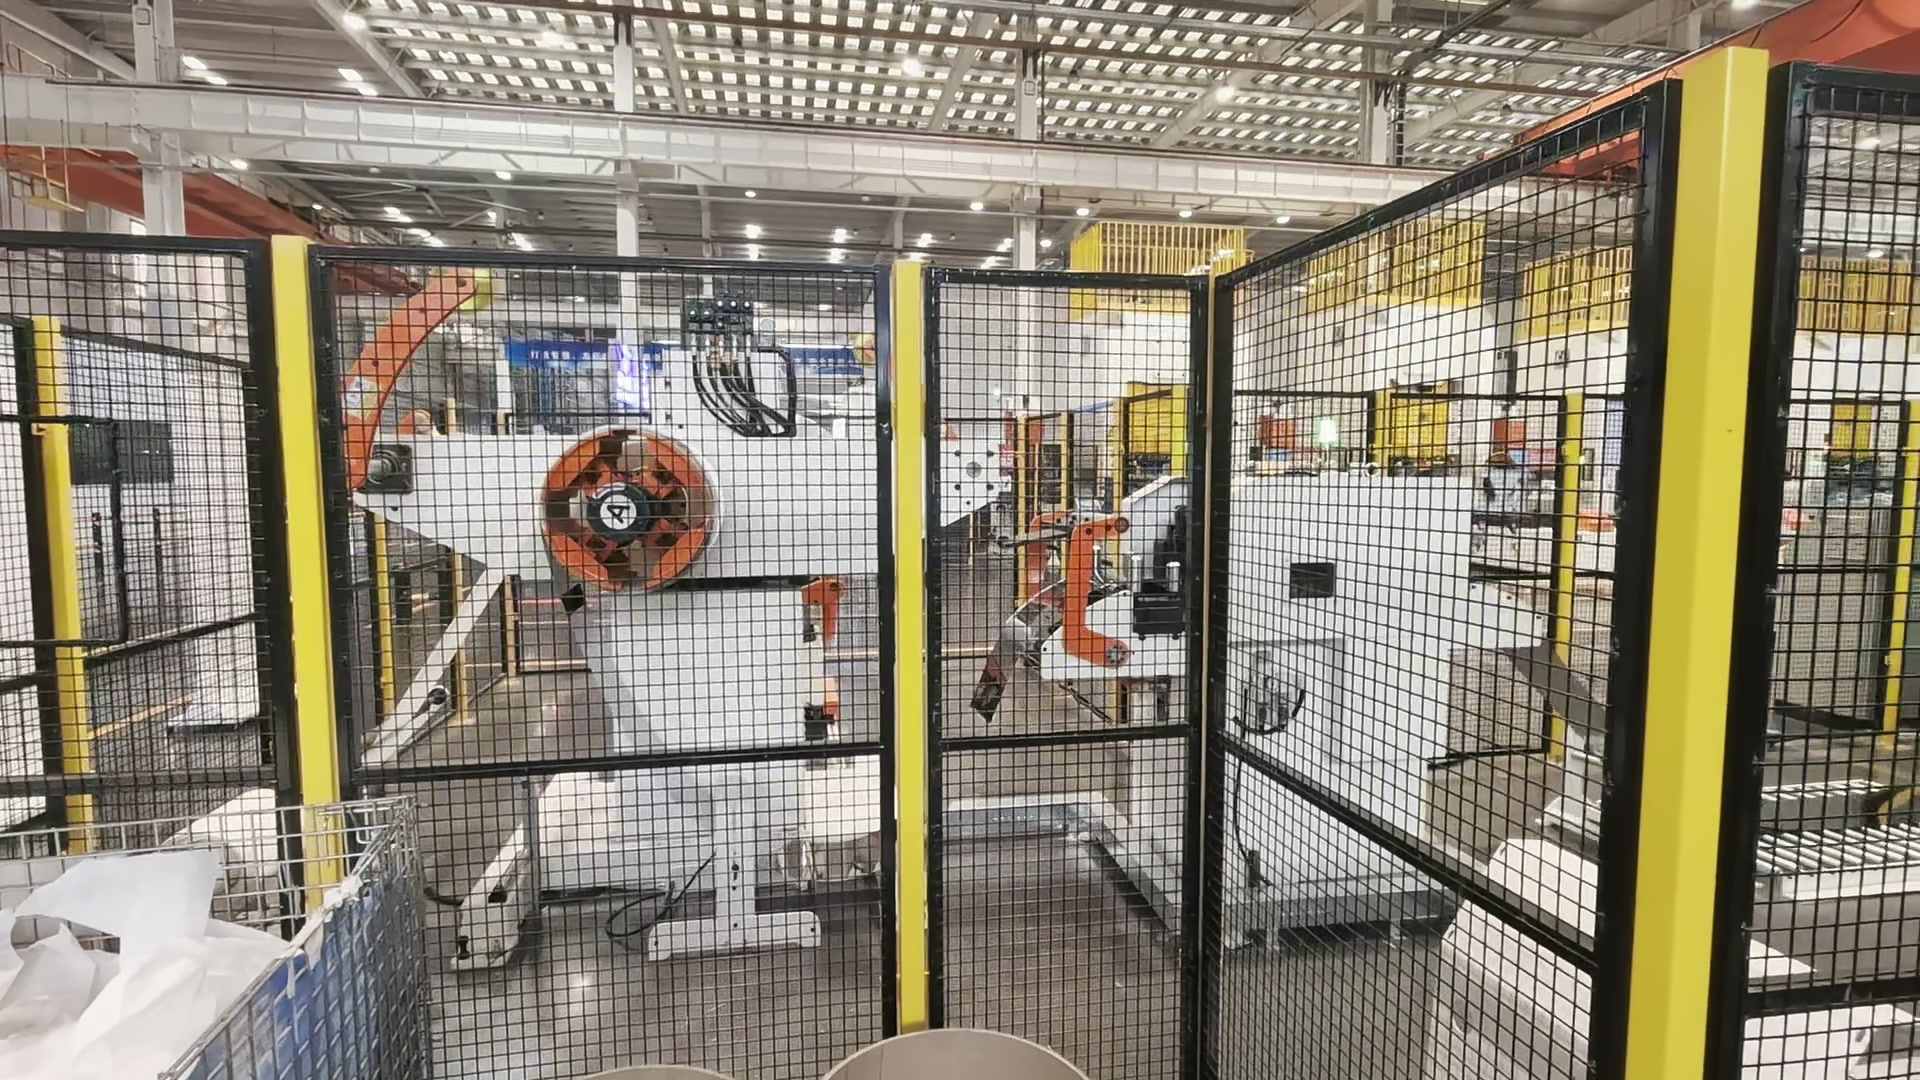
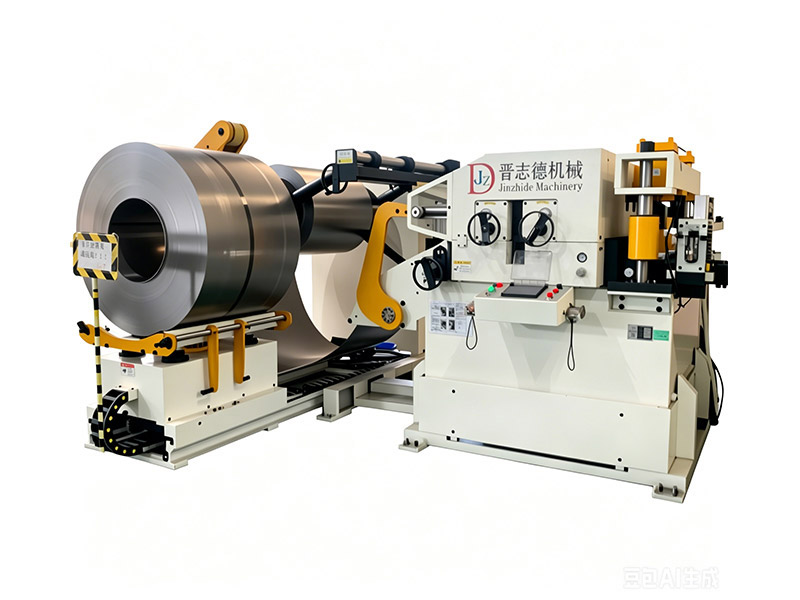
One feature of these washing machine drum stamping lines is the double head decoiler straightener. The decoiler carries two coil-holding mandrels. While one mandrel supplies steel strip to the line, the other holds the next coil in preparation for replacement. When the current coil runs out, the operator switches to the prepared coil following the equipment's operating procedure, which reduces the time spent preparing new material. On lines that process a large number of coils, preparing the next coil in advance shortens the waiting time between production runs.
After unwinding, the steel strip passes through the straightening rollers. Steel coils keep some curvature after winding and storage, and the straightening section uses adjustable rollers to reduce that curvature before the material reaches the feeder. The roller settings are adjusted for strip thickness, material properties, and the straightening requirement. On a washing machine drum stamping line, combining decoiling and straightening in one machine also simplifies the equipment arrangement compared with separate decoiling and straightening units.
Planning a coil-fed stamping line?
Send your coil dimensions, strip specification, and press data, and JINZHIDE engineers will review the decoiler straightener and feeding configuration for your application.
Get a QuoteServo Gripper Feeder for Continuous Press Feeding
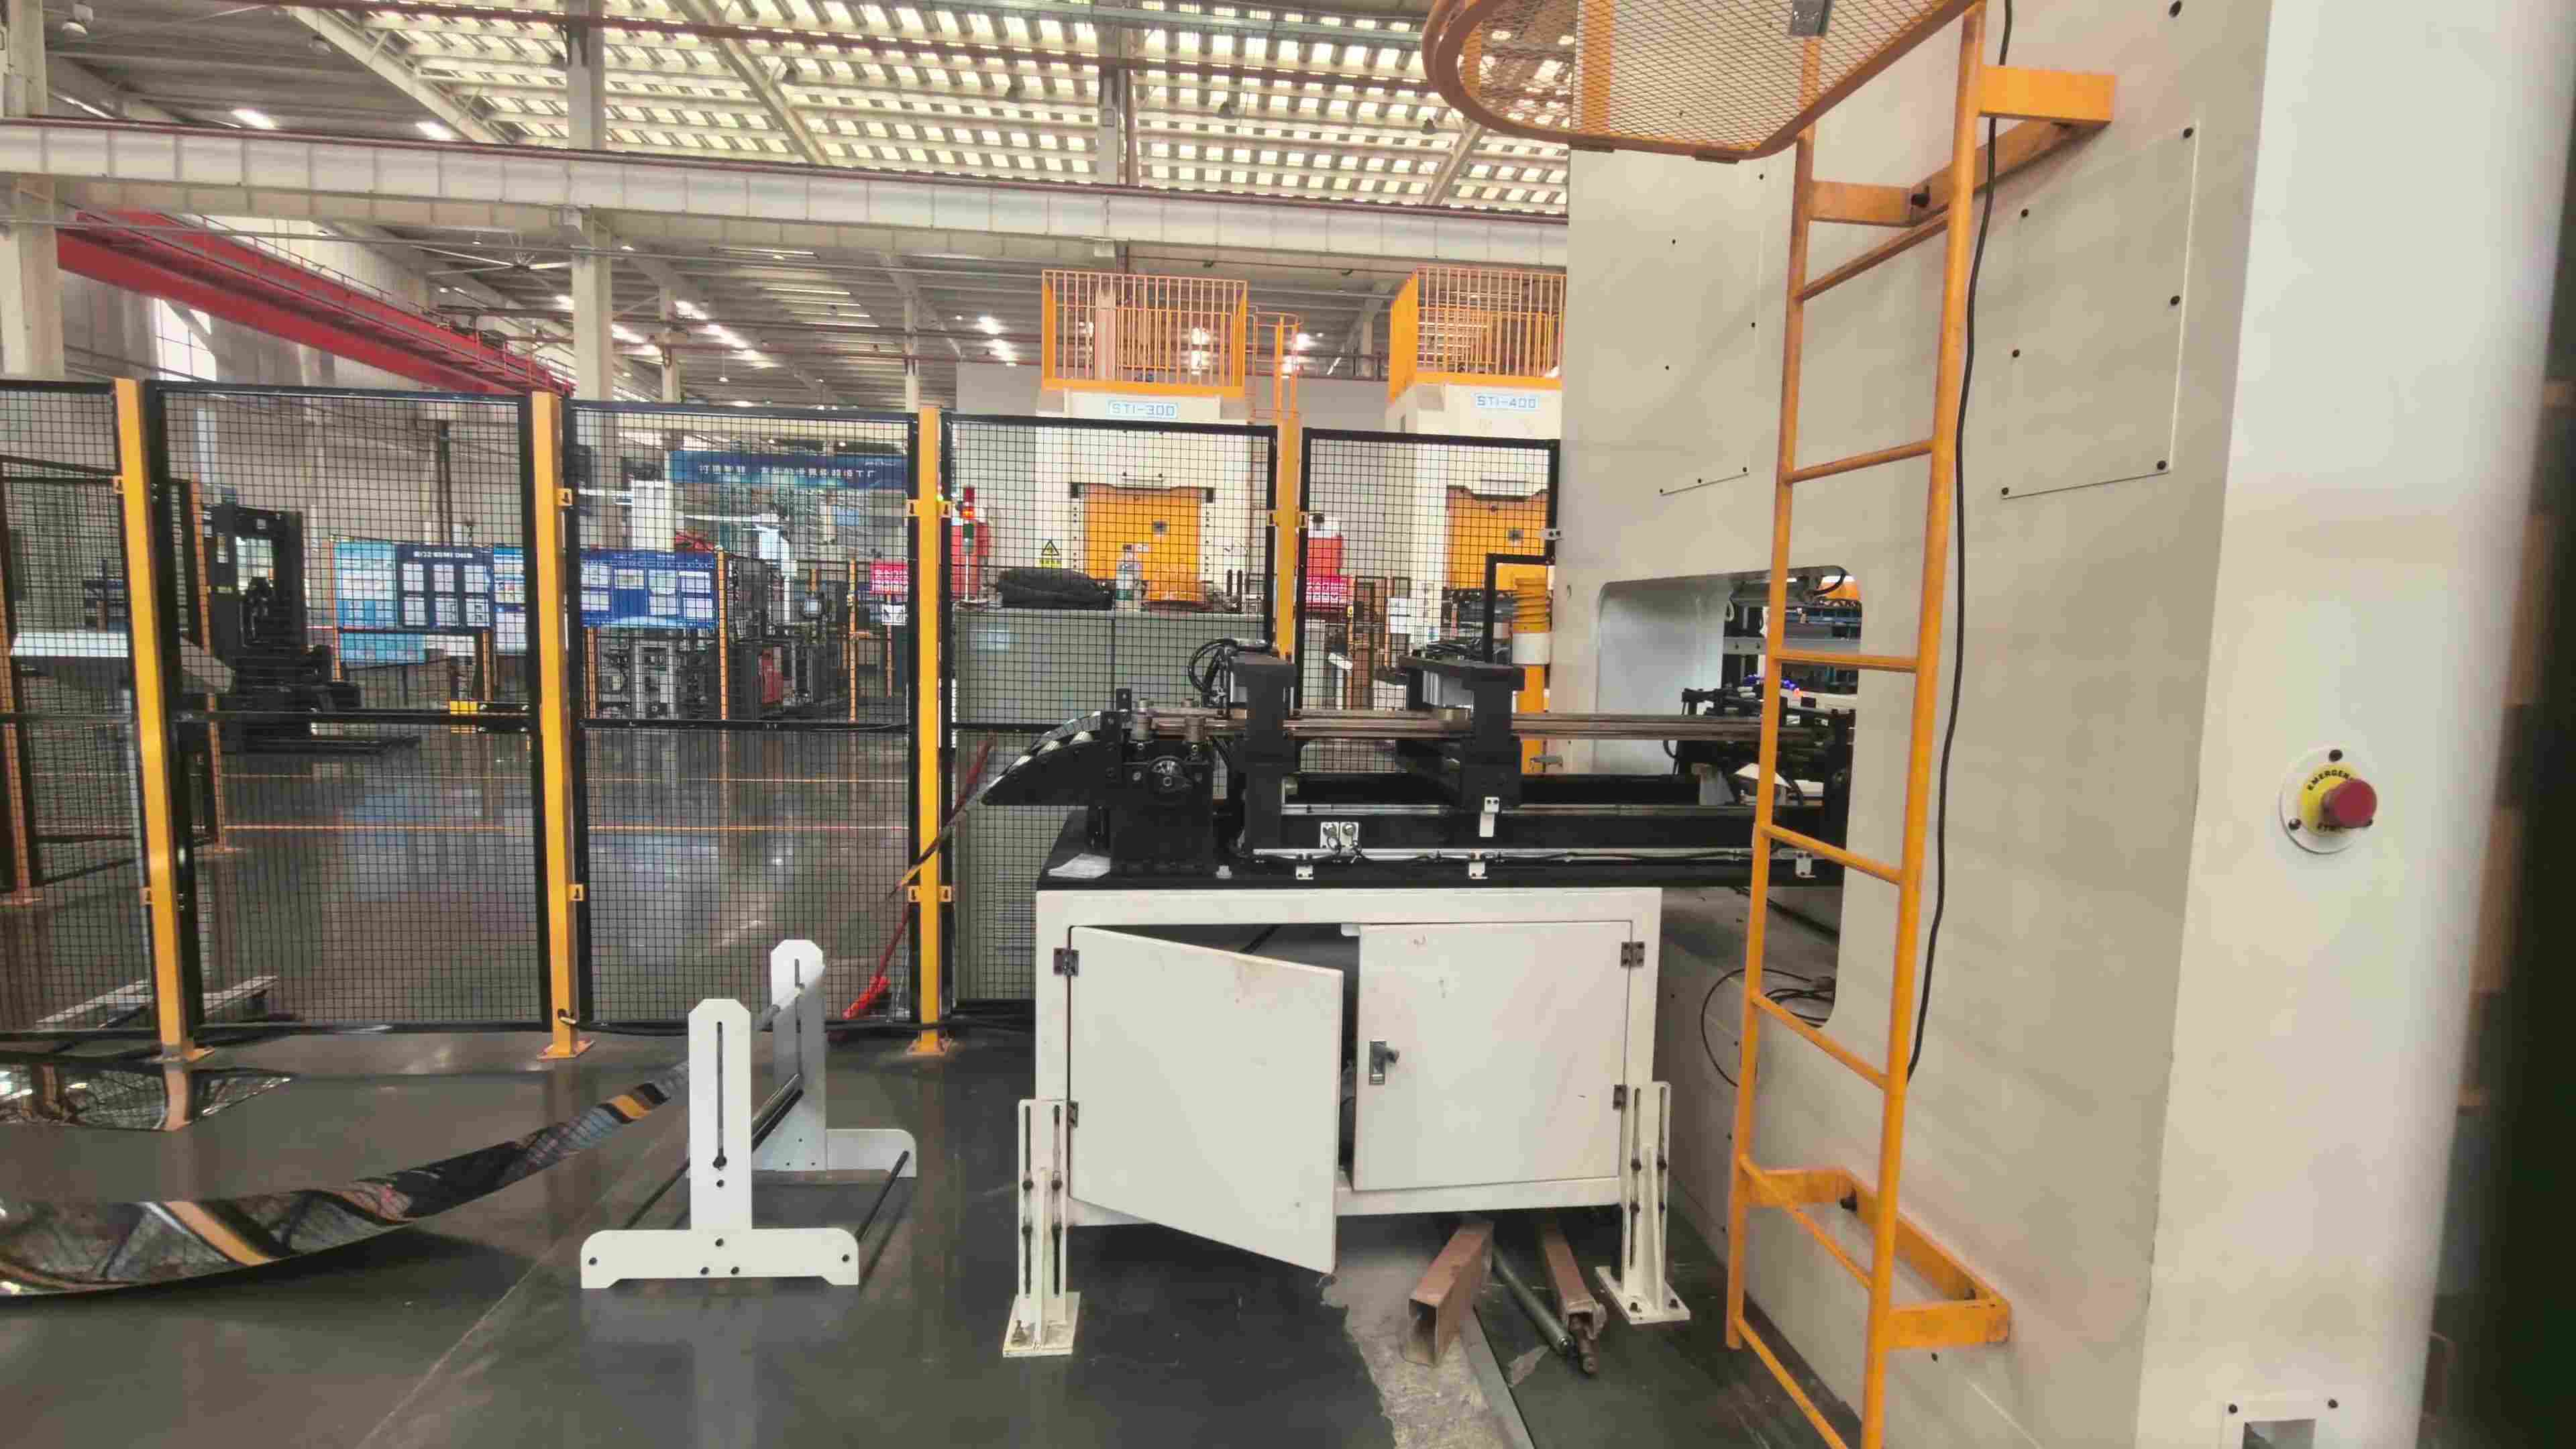
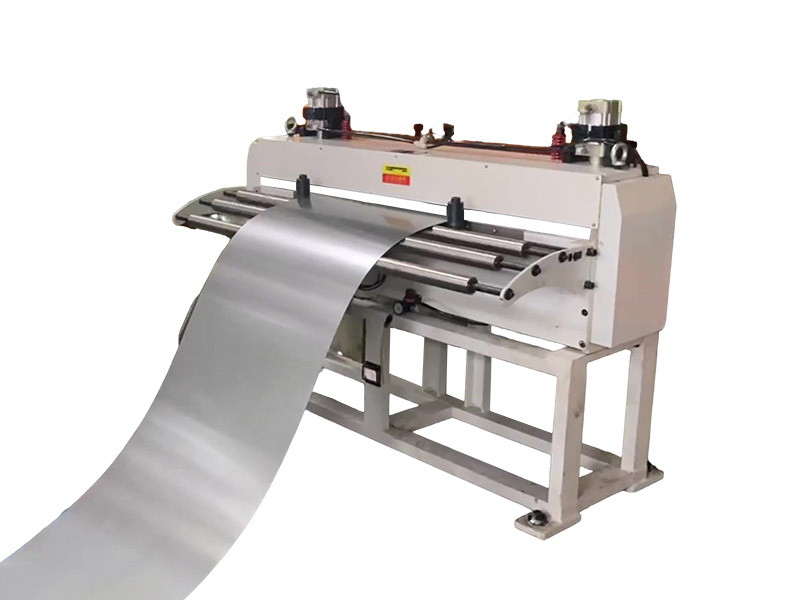
After straightening, the steel strip enters the servo gripper feeder. On a washing machine drum stamping line the strip is moved by a clamping mechanism: unlike a conventional roller feeder, the servo gripper feeder grips the material instead of pulling it between rolls. In each feeding cycle the gripper clamps the material and the servo-driven mechanism advances it by the programmed distance; the gripper then releases or resets for the next cycle. That movement is coordinated with the stamping press so the strip advances at the correct point in the press cycle.
Operators adjust the feed length and related parameters through the control system to match the progressive die. When the line changes to another product or stamping die, the feeding settings are adjusted to the new production requirements. On a washing machine drum stamping line the feeder provides controlled strip movement between stamping operations; actual feeding speed and accuracy depend on the material specifications, feed length, die design, and operating conditions.
400 Ton Stamping Press with Progressive Die
The steel strip is fed directly into the progressive die installed in the 400 ton stamping press. During production the feeder advances the material by a set distance and the press performs the required stamping operation; the process repeats as the strip moves through successive die stations. Depending on the die design, the operations include punching, cutting, and blanking to produce the steel sheets required for washing machine inner drums.
The feeder and the press must work together throughout the stamping cycle. If the feeding movement is not synchronized with the press, the material may be incorrectly positioned when the die closes. During commissioning, JINZHIDE technicians adjusted the feeding parameters and checked the timing between the servo gripper feeder and the 400 ton press. Feeding length, strip alignment, and the press operating sequence were checked during production testing, and with the equipment adjusted and connected the washing machine drum stamping line continuously processes steel coils into the required stamped sheet components.
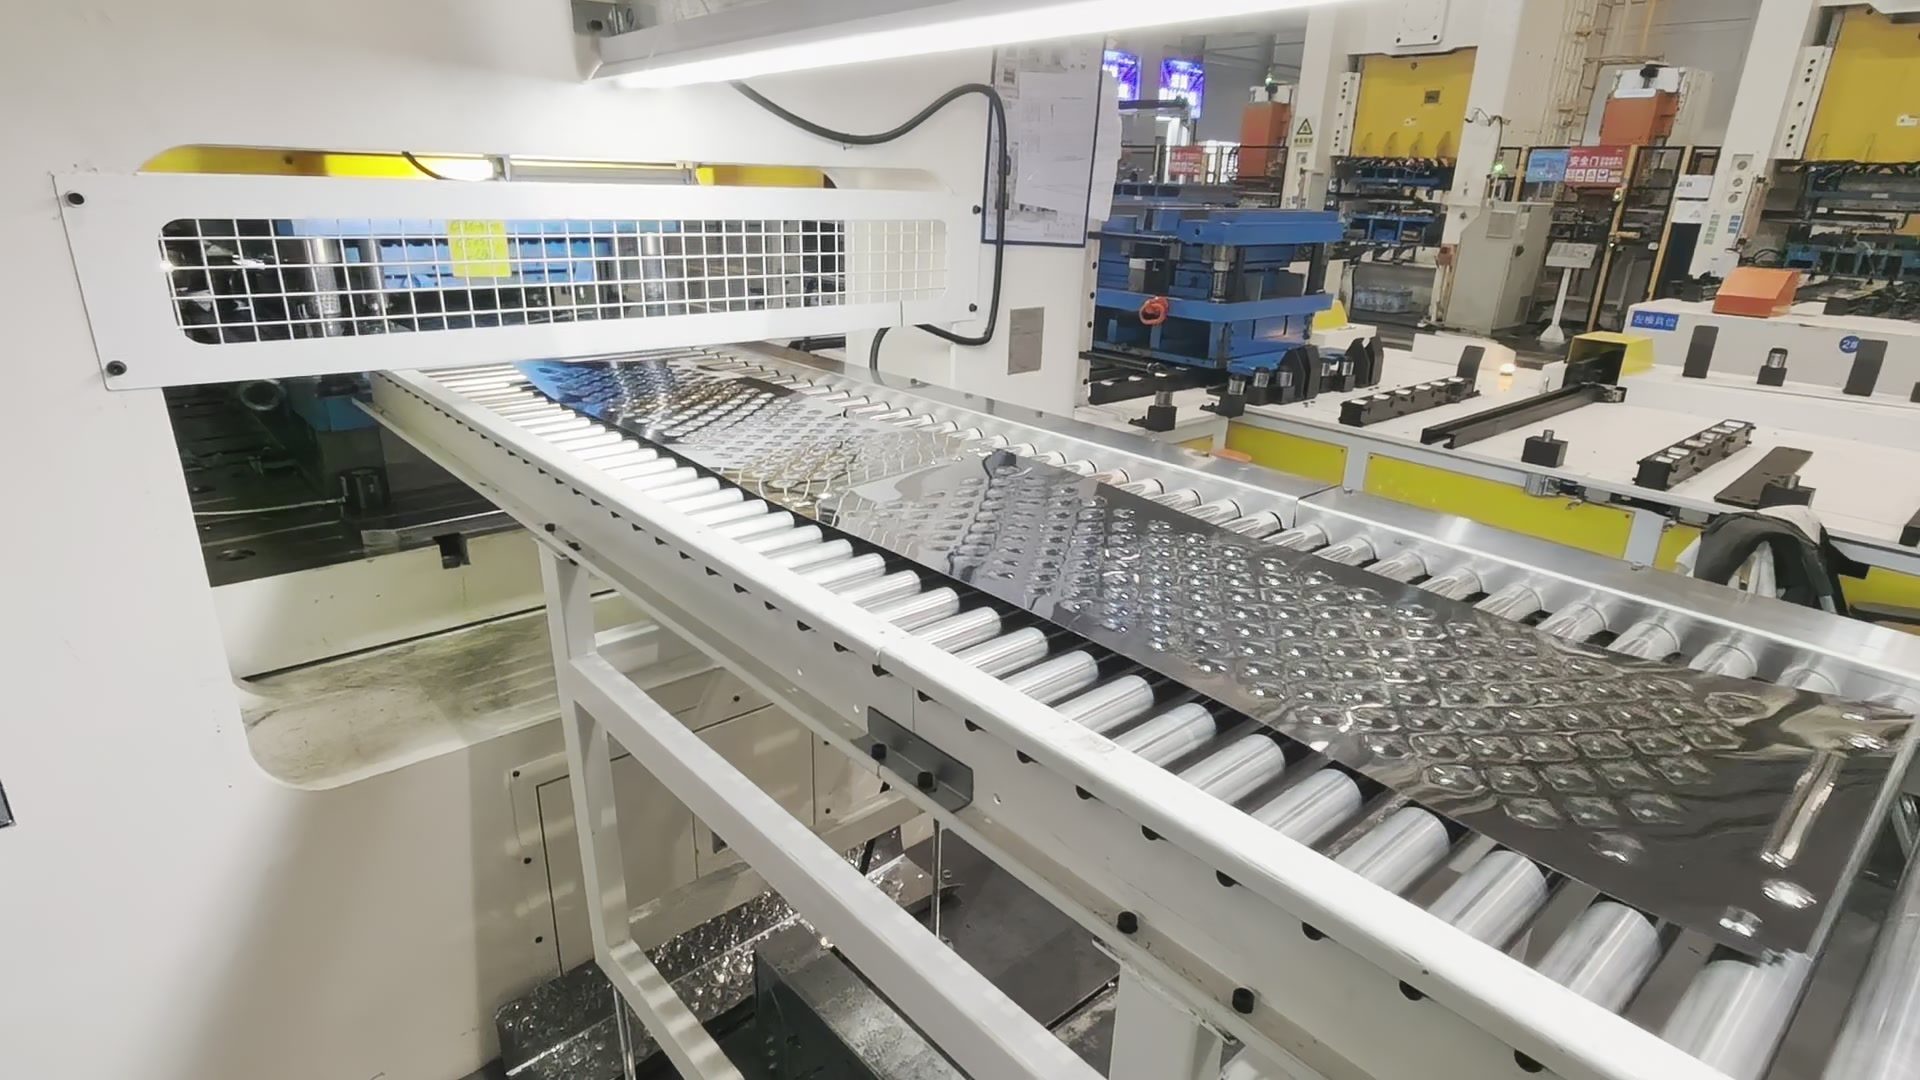
Installation and Commissioning at Midea Jingzhou Factory
JINZHIDE engineers traveled to Midea's Jingzhou factory to install and commission the two washing machine drum stamping lines. Installation began with equipment positioning and mechanical alignment, and the technicians checked the feeding centerline to make sure the decoiler straightener, the servo gripper feeder, and the stamping press were correctly aligned. After the mechanical installation, the electrical and control connections were completed.
The team then adjusted the feeder settings and checked the synchronization between the feeder, the press, and the progressive die. With both washing machine drum stamping lines positioned and connected, steel coils were loaded for production testing, and the technicians observed the material as it passed through the straightening rollers, entered the servo gripper feeder, and moved into the stamping die. Feed length, material alignment, and equipment operation were checked and adjusted according to the production requirements. After installation, adjustment, and testing, both lines were put into operation.
Need installation and commissioning support?
JINZHIDE provides site installation, feeder adjustment, press synchronization, production testing, and operator training for coil-fed stamping lines.
Contact UsEquipment Selection for Washing Machine Drum Stamping
For manufacturers planning a similar line, the equipment configuration should be based on the actual material and production requirements. The table below lists the information JINZHIDE reviews before recommending a decoiler straightener and a servo feeding system for a washing machine drum stamping line.
| Data item | What to provide | Why it matters |
|---|---|---|
Material | Material type and grade | Drives straightening settings and die clearance. |
Strip size | Strip width and thickness | Sets decoiler, straightener, and feeder capacity. |
Coil data | Coil weight, inner and outer diameter | Defines mandrel and coil loading requirements. |
Feed length | Required feed length per stroke | Matches feeder stroke to the die pitch. |
Speed | Required production speed | Sizes the feeding cycle and press working rate. |
Press and die | Tonnage, die dimensions, stamping force | Confirms press selection and line layout. |
The stamping press and the progressive die are considered together, because press tonnage, die dimensions, stamping force, and operating speed all affect the configuration. Washing machine inner drums are commonly manufactured using stainless steel, but the material grade and specifications depend on the customer's product design. Forming and corrosion behavior of the selected grade is documented in the technical resources published by the stainless steel industry association, which is why the material certificate and grade are confirmed before the straightening settings are fixed.
JINZHIDE reviews the customer's material specifications, press parameters, and die requirements before recommending a suitable decoiler straightener and servo feeding system for a washing machine drum stamping line.
JINZHIDE Coil Feeding Equipment and Technical Support
JINZHIDE is a manufacturer of coil handling and press feeding equipment based in Changzhou, China. The product range includes decoilers, straighteners, servo feeders, decoiler straighteners, and decoiler straightener feeders for metal stamping applications. The company also provides equipment selection assistance, production line layout support, installation, commissioning, and operator training. Press shop feeding and coil handling practices described in trade coverage such as stamping and coil processing reference material are reviewed with each project, since line layout, coil change routine, and feeder settings interact on a running line. Coil handling, feeding equipment selection, installation, and commissioning for a washing machine drum stamping line are handled by the same team.
FAQ
What equipment makes up a washing machine drum stamping line?
A washing machine drum stamping line combines a double head decoiler straightener, a servo gripper feeder, a 400 ton stamping press, and a progressive die, as on the two lines at Midea. The decoiler straightener prepares the coil, the feeder advances the strip by the programmed length, and the press with the die performs punching, cutting, and blanking.
Why use a double head decoiler straightener instead of a single head unit?
The second mandrel holds the next coil while the first one feeds the line, so the coil change is prepared in advance. On lines that process a large number of coils, that reduces the waiting time between production runs.
How does the servo gripper feeder stay in step with the press?
Feeding is coordinated with the press cycle: the gripper clamps the strip, the servo mechanism advances it by the programmed distance, and the gripper resets before the next stroke. The timing between the feeder and the press is checked during commissioning and again after a die change.
What happens if feeding and press timing are not synchronized?
The strip can be positioned incorrectly when the die closes, which affects the dimensions of the finished parts. Feed length, strip alignment, and the press operating sequence are therefore checked during production testing.
What data is needed to size a washing machine drum stamping line?
Material type and grade, strip width, thickness, coil weight, coil inner and outer diameter, required feed length, and production speed, plus press data such as tonnage, die dimensions, and stamping force. Washing machine inner drums are commonly stainless steel, but the grade follows the customer's product design.
Does JINZHIDE install and commission the line on site?
Yes. On the two lines at Midea's Jingzhou factory, JINZHIDE technicians handled positioning and alignment, electrical and control connections, feeder adjustment, synchronization with the press and die, production testing, and operator training.
The two washing machine drum stamping lines at Midea's Jingzhou factory are now in operation, with the double head decoiler straighteners, the servo gripper feeders, and the 400 ton presses working together for continuous production. If you are planning a washing machine drum stamping line or another coil-fed stamping project, send your material specifications, coil dimensions, and press requirements to JINZHIDE, and the team will review the feeding equipment that fits your production line.
Request a line layout review
Share your part drawing, coil specification, and target output. JINZHIDE will reply with a feeding configuration and equipment recommendation for your stamping project.
Get a QuoteSources: stainless steel industry association, applications reference; stamping and coil processing reference material.